One Welder to Rule Them All---HAPPY BLACK FRIDAY..

Hi guys

I know nothing about welding, but saw this on sale and bought it today Canadian Tire 179.00 CDN or $140 USD. Not attached to it., What should I be looking at. to keep an eye out for?

If there is already a thread on here about this please point me to it...

Is there a welder that can do everything on the plane, Gas torch or Tig?

Do thin aluminum for gas tanks and weld steel tube for the fuselage?

Thanks guys...happy Black Friday


120 volt FEATURES
  • Mastercraft Mig and Flux Welder can be used for both MIG and flux core wire
  • Infinite wire speed control
  • Four setting heat selection
  • MIG and flux core polarity control - quickly and easily change polarity settings
  • High-efficiency transformer
  • Thermal overload protection with light
  • Drive deck with dedicated power supply - helps to maintain constent wire speed
  • 2-in-1 spool holder, spool adaptor for 4" (10 cm) and 8" (20 cm) spool wires
 

Attachments

  • photo4106.png
    photo4106.png
    323.2 KB · Views: 0
Last edited:
The one pictured is a wire feed welder, typically MIG process. While some folks have built planes with MIG, it’s not common.

Welding is a pretty religious subject. Gas welding is usually oxygen and acetylene combined and lit into a flame. That’s what you use to melt the weldable material. Then you feed filler material in through the side. Mostly used with ferrous metals, but can weld aluminum with special prep.

MIG (above) and TIG are arc welding techniques where you use electric current to generate the heat. MIG feeds the filler through the torch head. TIG creates an arc and you feed filler material from the side, a lot like gas welding, except different heat source.

In my opinion, if you’re searching for the one welder that is the most flexible, TIG is a viable contender. But the buy-in can get up there fairly quickly. There are different levels of TIG, too. Features generally drive the price.
 
WUN-
Generally- the more kinds of materials you can weld the more money you have to spend. If you want to be able to do aluminum and steels--- (at least for aircraft construction)
you will want an ac/dc tig machine. (mig has been shown to cause structural problems in tubing for aircraft) The one you show - might be fine for non-aircraft use. You want to look for
an all steel drive system ( wheels) and availability of those as spare parts. (no zinc or aluminum parts please)

In a Tig machine you have 2 styles---- inverter style and transformer style. Inverter is MUCH smaller and lighter--- and has much more adjust ability for welding parameters.
The down side (somewhat) to inverters is that they are electronics heavy--- many circuit boards-- can be expensive to repair. Most weigh less than 100 lbs.
Transformer style--- large and heavy --- not as adjustable as the inverter. Few circuit boards...... can last decades with no issues.

In addition - Tig torches can be Argon cooled or water cooled. Water cooled torch never gets hot-- but the hoses are a little more bulky. Also needs water cooler.

The basic brand choices are Miller, Lincoln in the american brands. (miller supposed to have better cust svc.)
Pretty similar in function and features. Both good reputation.
Also a chinese model called "everlast". never used one --- they seem to work fine-- just dont know for how long and not sure about getting parts.

expect the smaller current models to start at about 2000 for transformer and 3000 for inverter.
The everlast - maybe 1000-1500 $ (american dollars)

I have a miller dynasty 200 ac/dc. Love it. would also be perfectly happy with a 180, 250 ( or 300) amp transformer machine too. (miller syncrowave)

Now-- you have to decide..... (the hard part) :-)
Tim
 
The MIG is handy for stuff around the yard, and for making jigs, but as the others have said, and has said Bob in the past, leave the structural welding to TIG or OA.
 
I certainly agree with what the others have said. O/A or tig for the airplane. An AC/DC TIG will allow you to do aluminum and steel. I'm using a DC only so can't do aluminum. Truth be told I wish I was better with O/A, the I would have used that to weld my airframe.

Also with noting, most 4130 airframes built today are mig welded; certified and kits (except BH kits which are O/A). It takes a high level of proficiency and skill to safely mig weld an airframe but it is done everyday by professionals. I mig welded the seat frames for my plane just for the experience...I'd never try it on an airframe and I'm a halfway decent farm welder😉

There are good foreign made inverter welders that are available for a reasonable price. I'm using a Thermal Arc DC TIG machine that performs excellent. I like Everlast better and they have a cool multi process machine that may be a great option for someone that only wants one machine.
 
The one pictured is a wire feed welder, typically MIG process. While some folks have built planes with MIG, it’s not common.

Welding is a pretty religious subject. Gas welding is usually oxygen and acetylene combined and lit into a flame. That’s what you use to melt the weldable material. Then you feed filler material in through the side. Mostly used with ferrous metals, but can weld aluminum with special prep.

MIG (above) and TIG are arc welding techniques where you use electric current to generate the heat. MIG feeds the filler through the torch head. TIG creates an arc and you feed filler material from the side, a lot like gas welding, except different heat source.

In my opinion, if you’re searching for the one welder that is the most flexible, TIG is a viable contender. But the buy-in can get up there fairly quickly. There are different levels of TIG, too. Features generally drive the price.

Thanks for the reply, I also found your project very interesting and read your Expedition link.

I wanted to ask you a question to make sure I understand your terminology when you say climbing cut for making router created ribs. Is that to mean feeding the material toward the cutting edge rather then away from it?

Michael in Toronto
 
Good question. When you’re routing, you can go one of two directions. One direction will tend to naturally pull you away from the form, and the other will naturally will tend to pull you toward (climb toward) the routing form. When using a climbing cut, you don’t have to force the work piece against the form (as much). It naturally tends to take care of itself. Don’t get complacent, though. It’ll get you. ;)
 
Mig has been used on air frames- WITH A GIANT CAVEAT. In the case of Mooney they take the entire fuselage and place it in a oven and heat to some temperature. The cheapest and most versatile process is oxygen acetylene. If you do go oxy/acetylene you want small torch tips - not the size that comes with a victor home depot set.
In the smith line of products I have found the small aw201 for tubing to be about right. I also use the aw203.
AW 200 Series (Acetylene)
 
In addition to Stan's Smith Airline torch (a fine torch), the Meco Midget torch is also popular. Both great tools for welding airplane parts.
 
IMO the best method of welding an airframe for an amature welder is O/A. It's hard to screw up a gas weld that 'looks' right. It's not difficult to TIG weld and do it right but it's also easy to do it wrong. If I were prepping to weld a fuselage I'd go handle a few torches, pick the one I liked the best, buy some RG60 rod and start practicing.

sjt, the caveat may apply to Mooneys but it doesn't apply to Maules, CubCarafters, KitFox, American Champion, Just, and Rans. Probably others too.
 
If welding is a religion, I have been discipling with the Church of O/A since late spring. My "pastor" got me switched on with Smith's AW1A and I've since sold the meco rocket in favor of the zen-like experience that Budd Davisson describes. I agree with Jon that if it looks good, a gas weld is probably ok. Where a good TIG bead might look machine-perfect, a nice, low-profile line of tight ridges from O/A (under a skilled hand!) is a work of art.
 
Mig has been used on air frames- WITH A GIANT CAVEAT. In the case of Mooney they take the entire fuselage and place it in a oven and heat to some temperature. The cheapest and most versatile process is oxygen acetylene. If you do go oxy/acetylene you want small torch tips - not the size that comes with a victor home depot set.
In the smith line of products I have found the small aw201 for tubing to be about right. I also use the aw203.
AW 200 Series (Acetylene)

Is the small tip oxy type welding also good for doing the gas tanks or is that a whole diffeent type of welding?

Michael in Toronto
 
Is the small tip oxy type welding also good for doing the gas tanks or is that a whole diffeent type of welding?

Michael in Toronto

I think gas welding is the best way to build your fuel tanks. That said, I TIG welded my tanks. Gas welding aluminum is more difficult that welding steel and it takes special equipment. In particular lenses in you goggles and aluminum welding flux. Also the pro aluminum gas welders use hydrogen and oxygen vs. acetylene and oxygen. The other issue is that a lap joint weld, like what is laid out for the Bearhawk tanks is difficult to do with gas and not have a lot of distortion.
 
I bought an Everlast TIG machine a couple of years ago (a model 250EX) because my OA skills had degraded excessively thru the years. My neighbor kid recommend Everlast. He has and Everlast and uses it for building motorcycles and stock-cars. So I then found out that my TIG skills suck too, especially when I know that a given weld will be responsible for keeping me alive. I have done my own fuselage tacking, some with OA and some with TIG.

So I made arrangements to get some help with my critical welding; I talked one of the welding instructors from the local technical college to stop in from time to time and finish up my welds. This welder happens to be an attractive young lady, about 37 years old. My wife usually feeds her well too (The way to a welder's heart is through their stomach). She has worked full-time in the aviation industry and (sad to say she is therefore quite busy) also welds and supervises the welding program at a local shipyard. And ... my professional welder also happens to own an Everlast TIG machine which she uses in her own home shop. For some unknown reason she says that she likes my machine better than her own... "It is smoother".

I bought a smaller gas-cooled torch for mine (which came with a bigger water-cool torch). The water-cooled one worked fine; I just connected it to a garden-hose which I ran on the lawn, but it was a bit bulky for getting into tight corners. The little gas-cooled unit has light/skinny hoses which makes it very user friendly. I also bought a bunch of cups/collets/lenses/etc off of eBay really cheap. I have less than $2K invested (inc the tank). When I bought mine I had been shopping around the country looking for the best deal. A sales-rep I was talking to was just too honest for his own good; he told me about a "special-deal" that the US distributor was offering via some obscure link on the Everlast web site, so I save a bundle there. I hope to get a sizable amount of that investment back in a few months by selling the machine when my Patrol is done.
 
A word of caution about using tap water for cooling TIG torches; the coolant flows through the hoses and the copper torch head. Minerals in tap water accumilate over time and become conductive. DC TIG will be least affected, except that you'll notice arc initiation will become more difficult, because the HF starting current will create a path to your faucet. AC TIG will become very unstable and depending on available ground paths, you'll notice much higher current demands, due to leakage to your plumbing. And then, forgetting to open the faucet usually ends up in a melted hose. Leaving the faucet on results in a big muddy puddle.
If you're in a warm climate, use distilled water in your cooler. If freezing is a possibility, use TIG coolant. It's got lubricant, in addition to the antifreeze propertiies. Actually, the purpose made coolant is always the best choice, in any climate.
When I did service work, I hated water cooled systems. Always a leak. Hoses were hard to change. Wrong coolant or tap water problems..etc..etc... But the weldors loved water cooled torches!

Bill
 
Interesting ... never thought of that. For what little I used/will-use tap water for my welding, it probably will not make a difference. Besides, I now have all plastic plumbing in my house. Pulled out all the copper a couple of years ago. We have our own well, and the water has only a touch of iron in it (no calcium and such so is quite soft). So the water eats up metal, first dissolves all the zinc out of copper leaving behind a crumbly copper sponge. Bathtub faucets last about 5 years. Water heaters last about 1 month beyond their guaranteed lifetime. So our whole-house copper piping was getting dissolved down to nothing, springing a new leak somewhere every couple of months. The good news is that the salvage value of the copper piping removed more than paid for the new Pex tubing I installed.
 
My understanding of the "mig on airframes" problem was not the particular welder or what plane--- but just how the Mig interacts thermally with the tubing. basicly
the same reason OA is considered the by some the best. High Carbon steels react to cooling by changing their grain structure to form a very hard steel. The more rapid
the cooling from a red heat- the harder the steel. Mig is a very rapid method to make a weld. Quick to start and quick to cool. OA heats slowly and cools slowly.
The heat effected zone is the transition zone between heated and non heated areas. the faster the heat/cool the narrower that zone. When it gets narrow with Mig----
that causes brittleness on the heat effected zone. When it gets hardened - that caused premature fatigue cracks to start there and the tubing can fail as the crack propagates
down the length of the heat effects zone. An OA anneal cycle can remove the problem by making the heat effected zone wider and softening the brittle zone. i think thats why
the whole-airframe anneal in a huge oven is done. Cant imagine how THAT sames time or money. ! I remember one of the rag+tube builders (i want to say maule-) used
Mig--- but them later they had recalls to repair cracking joints. Another problem with mig is that there is no way to "taper-off" at the end of the weld. You normally get a little
fat bulge at the end of the bead. That bump often has a pit or an "ugly place" there. That area can cause a crack too. Mis is best when welding low carbon sheet metal.
The OA guys like OA because it is slow on and slow off--- and usualy need no post weld anneal because of that. Tig is cleaner overall- but has a narrower
heat effected zone-- but its said for tubing less than .0125 wall--- it is not severe enough to call for a torch anneal. Thicker than 1/8 - post weld anneal
recommended.(after TIG)
Mig is best suited for low carbon sheet metal. ( IMHO) ----

So far between Tig, OA and stick---- can do anything I have needed to do--- never needed mig so far....
For high volume production on low carbon sheet steel--- MIG is the king.

Thats my brain dump on MIG ----
T
 
Last edited:
In the '70's, HSLA steels were becoming more common in more industries. At the same time, MIG welding was also becoming more commonplace in fab shops. The equipment was expensive and awkward, but the process was fast and less skill intensive than SMAW (stick welding) and Oxy-acetylene, which was becoming a rare artform - everywhere but the aviation industry. I've been in fab shops all over the country and several in UAE and I can confidently say that you'd be hard pressed to find many weldors versed in O/A welding today. SMAW still enjoys wide use, but not in production environments. MIG was taking over, painfully in some cases, but take over it did. Early on, only a few MIG wires were available. ER70S-2 was commonplace for high quality production piping and ER70S-3 was the less expensive choice, for mild steel weldments. Remember my statement about HSLA becoming more common? Well a new wire was introduced for welding the 4000 series steels. Initially, it was sold as ER70s-1B. This was sort of the infancy of MIG welding and the AWS hadn't adopted standards for HSLA wires. That wire came to be known and sold as ER80s-D2. It's a moderately deoxidized .5% Mo wire, that was developed specifically for welding 'hard to weld' HSLA steels. Today, there are lots of special chemistry mig wires available and even more flux cored and metal cored wires suited for any application you can imagine.
Whew! Can you believe I typed all that to lay groundwork to support the position that MIG is very well suited for welding HSLA steels, in addition to low carbon mild steels. One only has to look at the automotive industry to see lots of MIG welding HSLA weldments. Ever seen a 1000# roll of MIG wire? Yep, it's done. There are some programmable waveform MIG power sources that produce welds that would pass for TIG. Dan Denney (Kitfox founder) had a welding industry background. To my knowledge, every Kitfox out there was MIG welded, exclusively. Lots of planes have been MIG welded. While post-weld heat treatment is a method of stress relief, it's not the only method. I once had a conversation with a metallurgist, about TIG welding 4130 race car chasis and aircraft fuselages, without post-weld stress relief. He laughed and suggested that the vibration of the engine effectively stress relieves the structure more effectively than heat treatment would. I couldn't argue with that... Vibratory stress relief is not unheard of in industrial applications.
Now, I have to say that I would NEVER suggest that anyone MIG weld anything on an aircraft, unless you're a very accomplished and knowledgeable MIG weldor, with some well maintained quality equipment. While it's easy to weld a couple of pieces of angle iron, to make a flower stand, welding 1/2" x .035" tube clusters is a whole different animal! It takes a highly skilled weldor, using the right equipment and consummables. The process and procedures are tested, qualified and adhered to.
Now, to the original point of this thread: welders (the machines) are like a lot of things. Inexpensive ones don't perform as well as higher end ones. Machines that "do everything ", don't do anything particularly well. I know a lot of DC only TIG welders have been sold, but to my way of thinking a TIG welder should be capable of welding most any metal. Only AC/DC power supplies can do this in workshop environments. And yes, I'm aware that aluminum can be welded DCEN, but not without some very special procedures.
If you're wanting to be a weldor (person who welds) and make flower stands, a welder from a big-box store should work fine. If you're wanting to weld on any aircraft parts, I'd strongly suggest speaking with a knowledgeable welding distributor. Note that I said "knowledgeable". Just because the company has 1,000 locations, doesn't mean your store has a knowledgeable rep. Get a quality welder and ancillary equipment. Then practice, practice and practice some more!

BTW, I spent 42 years in a family welding supply business. Attended every darned class possible, conducted by Airco Welding Products, Miller Electric and Lincoln Electric. I was the 'tech guy' who did the process and procedure recommendations and serviced the stuff we sold, for a long time. After the supply business, I did consulting for a few years. But, in all that time, in all those places, I NEVER, repeat NEVER! Never did I ever meet a 37 year old attractive young lady weldor!

Bill
 
"37 year old attractive lady welder" ..................... Im waiting for pictures !
I KNOW there must be some out there ----- but never met one..... seen some on youtube. But they could be just stunt doubles ! :-)
Tim
 
but seriously folks.......
If you THINK jyou want to buy a Tig machine.....
Find someone who has one that will let you try it for 10 or 15 minuites. You will know if you enjoy it or if you find it impossible. Only if you enjoy it buy a machine.
because it will take a lot of hours to get OK with it. If you enjoy it - those hours will go fast. If you hate it --- you will never have the patience to get good.
Seems like people either love it or hate it.
Tig can do anything mig can do--- and do it way better. just not as fat or as cheap.
People who have reported on the everlast units seem pretty happy with performance. The expected failure mode is if a circuit board blows--- can you get one.......
or do they suggest you throw away the whole machine......
Of coarse there ARE used miller inverters out there that are sitting unuse dbecaue they blew a board and no one want to buy a new board - maybe for fear
that if they replace the bad board they will find it was really multiple bad boards........ No perfect solutions I guess.
T
 
Yep! Point made. I'm thinking that The Blonde wouldn't take too kindly to having her as my workshop helper...

Bill
 
Thanks Chris. I've been 'away' from the welding industry for a lot of years now. Still get calls from old customers, who became friends. I light up like a light bulb, when aircraft come up! But I really light up when I hear talk of welding! I still can't walk past a weldment and not critique the process and procedure... Unfortunately, there's no medication to quell that. Something I've learned, however, is to avoid conversations about religion, politics and welding. Welding, I've found, can be more inflammatory than the other two. I know this and swear it's right. But I'll happily argue with a stop sign...😎

Bill
 
A buddy lent me a TIG machine last week. I'm hoping to get good enough to tac weld only for a pro to come behind me. Tabs and non structural stuff only. I'm an "o.k." stick/mig welder but so far I swear this TIG machine is broken! :) As mentioned by someone else, if you haven't tried it, I'd try it before buying a machine. I have a pro coming this week to hopefully show me how it's done. Maybe I shouldn't have started my first attempt on thin wall sheet metal. Somehow I'm hot enough to make a hole but not getting the filler rod to melt with it. Hopefully successful instruction later this week!
 
Wyatt Swaim told us in class that a TIG won’t absorb a MIG tack. I don’t have any experience with that, though. Will O/A?
 
Wyatt Swaim told us in class that a TIG won’t absorb a MIG tack. I don’t have any experience with that, though. Will O/A?

Your instructor was absolutely correct. MIG and TIG welds won't mix. That is my experience and not here say.

I have had luck using silicon/bronze TIG rod to work around a MIG weld. S/B is also good anytime I have a difficult or very thin piece to weld.

I changed from air cooled torch to a water cooled torch. I use a submersible pump in a tank for coolant. The pump was about $80 and the tank was a plastic storage container. I find that I get better welds with a water cooled torch and I don't need to wear a glove.
 
Last edited:
Chris,

I'm telling you: Welding can stir up more controversey than politics! It's a real mixture of science, art and lots of Voodoo. Any of those 3 is wide open to interpretation and 'discussion'. Man, do I love a good 'discussion'!!! :cool:

Bill
 
Mot sure what he is refering to about Tig "over" mig. Mig wire is commomnly ER70S6 and tig wire is usualy ER70s3--- only difference being the elements added to absorb
various contaminants. I have Tig welded plenty of thin ( paper thin) steel with the mig wire. welds fine and is supposed to flow a little better than the S3 version.
Is Swain referring to some chemical incompatibility ? OR -- is he talking about the HAZ situation that the fast Mig tack created and that the TIG bead going on over it doesnt
completely anneal the area ????

Brad---- do NOT dispair---- its easy---- once you learn where to put the machine adjustments.
Try about 13 CFM argon...... keep a short arc length (1/16) --- for steel ( like 3/32) adjust to about 50 amps--- go slow and wait on a puddle. Dont overheat-- be patient-
when the puddle get to be about the size of a BB- then make a dip. Keep the end of the rod about 1/2 inch forward of the puddle.(must keep the rod in the argon too so the
end doesnt oxidise) --- move forward with the arc about 3/32 and stop and wait for another puddle.... rinse and repeat...... Just weld in little tiny steps when you are beginning.
One droplet of rid in each puddle--- the droplets overlap about 1/3 with their neighbors. On steel go slow-- wait for the puddle- dont floor it (amps) -- Keep you arc length
short and dont touch the tungsten to the work or the rod.

Doing aluminum--- you WANT to floor it and move along. For stainless ---- you go even slower than with steel. might take 10 or 12 sec. to get a puddle without overheating.
(which is REALLY easy with SS)

Its really pretty easy - but having someone to show you really speeds learning up !

T
 
Fairchild - Thanks for the tips! I was going to make a joke in the post about "surely this machine is broken." :) I usually do pretty well at something I want to do, but all I made was holes in thin metal. The good news is....., it was broken! :) I had a pro come by today to show me how to do it and he scratched his head for 30 minutes trying different settings. Kept fowling the tungsten like I did. But his was a much prettier fowl than mine :). Last resort, he swapped the leads plugging into the machine and Walla! I must be wrong, but I checked the maual and swore it said the positive was supposed to go to the welding lead. It didn't. I asked him to weld examples of the several situations I'd be in (tabs on tubing, tubing to tubing, and thin sheet stringer brackets to tubing) and I tried a few practice runs after he left. Very relieved now that I think I can get dangerous enough to do my own (non-structural) welding after a little more practice. I knew it couldn't be me! :)
 
Because TIG welders are also usable for SMAW (stick welding), depending on what you were reading, you might well have read correctly. SMAW, when using DC current, is done DCEP (Dierct Current Electrode Positive). DC TIG is DCEN (Direct Current Electrode Negative).
Way too many acronyms, don't you think?

Bill
 
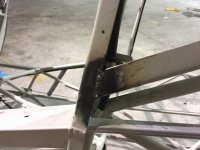
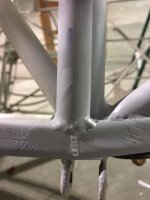
3 practice sessions and I welded (TIG) on my plane. Sounds pretty reasonable, right? Probably taboo to open yourself up to welding pics, but if anyone is interested, you can see some of this evolution on my build log. http://www.mykitlog.com/BradR/
 

Attachments

  • photo4164.jpg
    photo4164.jpg
    353.1 KB · Views: 0
  • photo4165.jpg
    photo4165.jpg
    512.3 KB · Views: 0
  • photo4166.jpg
    photo4166.jpg
    438.3 KB · Views: 0
Brad-
You will get better as you get more co-ordination and comfort doing it. Going around a tube will always be harder than just straight because your hand position for both hands
moves continuously. try to make all your motions and speeds very constant and machine-like. try to keep your arc-gap about 1 mm. (but dont touch :-) )

Yes- the torch should be in the Neg. terminal - but it may or may not be labeled like that on a Tig machine.
If you had it backwards on DC - all the heat would go into the tungsten instead of the work. On AC for aluminum--- the work heating happens on tungsten (electrode) negative-
and durring the reverse cycle when the tungsten is positive-- the current is sucking dirty gook off the surface of the work (cleaning it) and depositing said gook onto your tungsten.
(if you have it more than 50 or 60 % you can see the tungsten getting junked up fairly quickly- and it gets hotter too - to the profile of the tungsten may change)

On steel- watch the tip of your tungsten. If it gets blue- turn the gas up a little. If it gets worse - turn it to lower than the first setting. (I have found about 11 to 13 CFM) seems
to be a sweet spot.

Dont be afraid to grind the tungsten if it looks dirty or irregular--- or if the puddle starts fighting you. You can also clean the work with a steel tooth brush every few inches.

Also watch the end of the welding rod--- how it looks. If it gets out of the argon while the tip is hot- the end will oxidize...... then on the next dip it wont want to flow nicely
like you want it to. If you keep the work clean and a short arc gap it will all most just flow on effortlessly.

A fellow that was a very good welder that used to work for my dad..... we tried to employ convicts on work release to help them. He was telling me about trying to teach these
Gomers how to weld better. They would come and claim the welder was broken. (it was a stick welder) He would explain to them that the welder wasnt broken........
Then he would put a rod in the clamp---- bend the rod a little like a rocking chair bottom----- then he would lay the rod and holder down on top of a piece of flat sheet.
then he would walk over and turn on the machine. It would start welding and deposit the whole rod onto the sheet with no one even touching it. The he would hand them
the sheet with a perfect bead the welder made without a human even touching it. --- and say "the welder aint broke" ....
Similar to flying--- when you are shown that the airplane can fly ist self better than you can fly it (when you are starting and overcontroling it ----)

When you do a weld on your airframe--- you dont want a pit or a hole in the bead. Those can cause all kinds of problems. Usualy you want to grind the surface localy
and re-do the bead on those. Also another detail to avoid--- at the end of the bead the last dip can have a little tiny pit in its center. Dont want that as it can be a place for
cracks to start. When you get to the end of the bead.... cut the current down some and do some circular orbits around the spot where the pit forms- that will let the puddle
flow a little and wash in the pit and make that last bit nice and smooth. The inspector should gig you for any pits in your bead. The nice part is you can always grind however much
of the bead down and go over it again and re-flow it-- adding however much rod as needed.
T
 
I don't know about the rest of you folks, but I have been REALLY enjoying this master class in the finer tips of TIG welding. I keep reading things like "make sure you don't do this or you will have that kind of issue" and sure enough, that's exactly what happened to me and I couldn't figure out why. I had put my little Miller DIversion 180 aside after too many frustrating hours of making crappy welds and just bought more acetylene. Now i'm kind of pumped to break it out again and work at getting decent welds with it with my (largish) pile of scrap steel.

Thanks for sharing your knowledge, fairchild (and all you other master welders). It is really helpful to us complete amateurs (especially us software nerds: we're hopeless :-)
 
When I started welding, I taught myself to gas weld aluminum with Oxygen Acetylene equipment. Mostly an ego trip but I found that that skill carried over to TIG very well.

I did have special goggles and the proper flux. Because the goggles filter out red, you had to watch the metal as it changed with temperature and how the puddle was forming. Heat control and feeding the rod were critical to aluminum welding. When I then learned TIG, the transition was very easy.

When I was a kid, race car bodies were welded aluminum and that was what I was trying to copy.
 
Thanks Fairchild! I take it that little pit hole or two didn't get by you? The pictures make them look much worse than they are. :) O.K., I'll grind.
 
Brad- I have found that when I am trying to run a good bead- and I can see that the puddle seems to be getting a little dirty (when it resists flowing nicely) then the puddle will resist
wetting one side of the work--- and you move on---- that leaves a pit kind of defect there. It seems to be associated with the puddle not being completely clean. what that probably means is that
a tiny bit of air got to it as you were moving along. Could be torch angle, too little argon, using a gas lens on inside corner and making a vortex which sucks air in, and maybe other reasons
we cant even see. But --- when you see the puddle getting where its stops wetting ---- just stop--- use your steel tooth brush to clean it off, grind your tungsten for good measure--
then start again where you left off. you will see its is instantly better.

Also many times when I was learning-- if I held too big of a arc gap- that tended to make the puddle dirty- also it often gave a melt-through. The shorter the arc length the better
it will work. Try to keep it to 2 mm if you can. A short arc length will also keep those lateral edge gaps from forming. For thin steel tubing- use a small current with a short arc length
and be patient and wait for the puddle. Dont get in a hurry.

Something to watch for when dipping the rod--- when you dip- it is good to see the filler just added to the puddle wet forward a little. That is a sign that the puddle is clean and behaving
nicely. If it is doing that it is probably doing it sideways too- which is good as it tends to indicate it will likely be wetting into the sideways parts. On the other hand-- if you dip and you
dont see that nice wetting--- you may see that last dip draw up into a ball and just surface tension its self---- so if you see it stop wetting--- just stop --- brush the work, grind the
electrode and clip off the end of the welding rod. If you mess up and get the end of the welding rod out of the argon during the dipping--- the rod will oxidize on the red hot tip-
then on the next dip you may get the lack of wetting and surface tension thing starting. If the dips dont want to wet each side and forward---- something like that happened.

Accidently getting the rod out of the argon is very easy to do----- because you are often putting 150% of your attention on the arc gap trying not to touch the work-- trying not to
touch the rod to the tungsten- . you can practice keeping the welding rod as close to the arc as you can without the heat melting a liquid ball on the end of the rod. just back the rod
out a little at a time until its not melting the tip of the rod. This is useful for another reason---- when you dip the rod into the puddle-- that cools the puddle just a little. That allows
you to reduce the temp of the puddle. (to NOT overheat) Then you just wait a fraction of a second for the puddle to get liquid again for the next dip.

This is ALL SO MUCH EASIER if someone can show you this in person. I took a semester class at our local county tech school. It wasnt perfect--- but it got me started
on the basics and you had someone to ask questions of (when he wasnt swamped with the other 60 students) After that class I kept practicing for another 2 years
to refine my skills. During that period I got extra practice welding all kinds of stuff for other people and for work. That got me more practice in a short time which helped too.
gradually learned to weld thinner and thinner aluminum sheet. I can usually do .040 ---- maybe .032 on a good day. There are special cheats you can do when you get that thin too.
(like a thermally conductive back-up plate behind the joint.) or using a 50 or 60 % electrode negative setting (thats 40 or 50% cleaning) That helps keep the work cooler and the
extra cleaning helps prevent accidental holes.

Tig'ing is pretty easy and wonderfull once you get all the machine adjustments right and get your hands and feet synchronized. I also use a magnifying lens in the helmet.
My theory is that you cant weld any better than you can see. It seems to really help when you are trying to hold a very short arc gap. (which I always try to)

Hope this is encouragement for anyone who has a machine but got discouraged. Watch all of Jodys' vids at welding tops and tricks. He is really the greatest at teaching.
I like his technique WAY better than swain. I think Jody welds each day -every day - all day. You cant top THAT !!!! :-)

If anything I know helps someone---- what more could I ask for !
Tim

PS--- Brad-- if you see a weld you dont like-- fear not ! Grind it down--- but keep in mind- you usually dont need to grind down
to the level of the tubing--- your new pass will be re-melting whatever is leftover and it will integrate into the puddle. Most times you can
just grind about 1/2 way down. Its usually nice and clean after you grind. remember this is NOT like stick welding.
Stick welding fails often involve hollow pits or pits with glassy flux inside them. With those-- you often have to grind all the way down
to get the slag gone. For Tig-- you have no flux or slag. That makes things way easier to remedy after a boo-boo.
 
Last edited:
Great advice! Thanks for sharing your experience and expertise. I find myself watching Jody every day, sometimes several Vids a day. You’re right about his teaching style. He’s great to learn from. Always a little something different, and every type of welding imaginable on his site.
 
Jody is great. Everything you need-- nothing you dont. Then there is the tig finger. Got to order one of those !
T
 
I ordered mine recently along with a couple accessories. I hope I can get my shop going this holiday so I can get to using it!
 
One last thought i should mention----
A safety note--an IMPORTANT ONE.
NEVER NEVER use brake cleaner to clean parts for welding. brake cleaner has chlorine containing solvents. When that becomes exposed to the intense arc radiation (UV)
--- that breaks apart the molecule and it rearranges the chlorine into a new molecule known as phosgene. In case you dont remember that one---- it was developed and used
as poision gas used on the WW1 battlefields. One good breath and it dissolves your lungs and you die. Its really THAT bad. i have read of a guy that did it and had some
hiding in a crevice. when he hit it --- it transformed and he spent about 1 month in critical condition but bare survived. he figured it could have been just miligrams hiding
in the joint where he couldnt see it.

This applies to electric welding. As far as I have read... alcohol and acetone are OK to prep with.
I figured we cant spread this info far and wide enough......
Tim
 
I have been welding quite a bit in the last 3 or 4 years - kind of in spurts as needed--- but pretty heavily when "on"--- and I STILL learn stuff from Jody just about every time
I watch him. Many times he reminds me of a trick I saw from him a year or 2 ago and forgot about. I have been lately doing repairs to a set of 85 year old aluminum wheel
pants. They appear to have been run through rock back in the day. And just worn and chafed and all the tings old aluminum does after that many years. I re-remembered
one trick I used to good effect....
For thin and thin+dirty aluminum------- turn the cleaning control to about 50%. Start the arc but use a minimum current - dont create any melting. work and play the arc up and
down the area to be welded. This is sucking the dirty surface corrosion off the metal. Do this until the whole area to be welded looks frosty and even. Now you at least have a
non-contaminated surface. That gives you a big advantage towards getting that first dip to whet in cleanly. You MAY have to grind your electrode off clean as the dirt removed
from the work end up on the electrode tip. (and you want that CLEAN too- especially for that first dip to go well) Once you get the first dip cleanly and wetly attached- then its
MUCH wasier to get the next one in because that first one acts as a heat sink (to help prevent a melted hole) I usually let it cool for a moment after the first drop. Might even stop
every 3 or 4 dips for a few sec. so I dont overheat and risk a hole. When it get down to about .030 inch material im having to work hard to not get too hot. When you increase the
cleaning--- that reduces the heat into the work and makes the electrode hotter. That can be a bit of a cheat to help prevent melt through holes.... but also helps a lot on old dirty
material too. Only downside is that it sucks dirt up onto the tungsten like a vacuum cleaner--- so you may have to grind it more often-- but thats OK if it get you a good sound weld
where you might not have been able to do it otherwise without making aggravating holes !

Another trick I may have invented--- (but I bet somebody else thought of it before me--- cause i taint that smart-)
These things had a lot of old holes from previous riveted on patches. (ugly ones too) So I removed the patches leaving a bunch of empty rivet holes. Now- how to fill the holes ?
Normaly if you have a hole in really thin Al. sheet- you would try to lay the torch over sideways and melt it edge-on. But that always just makes the hole bigger really fast. and no way
to get the filler in there.... You can heat outboard the hole and make a doughnut a little ways outside--- let it cool and keep adding smaller doughnuts toward the center. at some point you still have to weld it edge-ways ... but at least its thicker now- you have a chance. But you end up with a little mountain of filler when you are done. It works... but lits of fileing.
( normally i weld up the outside till closed, Then I flip over- clean the back and make a matching inside bead- which will not get ground or filed down.)
So I tried a new method which seems to work and be easier to finish up. I find a piece of filler rod which just fits into the hole. If it a little too bit- file or drill the hole till it just fits.
Then I slip the rod in from the back side. The cut the rod off on the front with about 1/4 to 1/8 inch sticking out. Then I start the arc. heat a doughnut around the hole a little
out board of it. Then before it cools - jump to the rod stub and heat it till it starts melting down. It will for ma liquid ball as it does so. The ball gets bigger as it goes. When it gets down near the surface- heat just outboard the ball in a circle. The ball and the edges will start to blend. Keep moving in a circle- never stopping. Most of the time I can get a nice little shallow
dome of filler about the size of an aspirin tablet and about 1/16 tall. Some times I might let it cool and brush it and come back and add a drop or two more of filler it it needs more meat
or a spot that didnt zipper up 100% the first time. Then -- flip the work.... clip off the rod on the back side and repeat back there. Seems to be a lot less stress and much quicker than the other way.

Yes- I know this is a lot of yacking about an obscure little thing--- but i couldnt sleep from recovering from a tooth infection. So here I am yacking.... Havnt gotten out to the barn in a few weeks to make more ribs because of the cold weather and other jobs.
I have a small roper -whitney foot operated sheet metal punch. I am using it to rough-out the lightening holes in the ribs. But you have to stand on one foot as you are holding the work
in the perfect position- then stomp. I am trying to mount an air cylinder to make it operate from a simple electrical switch so I can sit down and keep better balance and not be exhaused
after 2 or 3 ribs. It has a 1 inch round punch so it takes about 20 hits to do 1 of the big holes. Kind of like a nibbler working. But it doesnt distort the material at all. I like that.

Hope to get back to it an a couple days when my jaw feels better.

Tim
 
Great hole filling tip! Jody also recommended pulse settings, too, to keep from overheating things like this. I’ll have to give that a try. I didn’t check to see if you can do pulse and AC at the same time on my welder, but will.
 
Back
Top