Bending steel for fittings

Frank

Well-known member
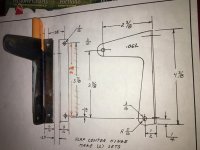
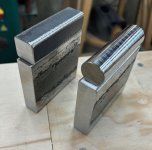
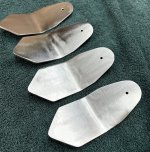
As I practice oxyacetylene welding, I’m also thinking about forming the steel parts needed for the wings - the next steps on my LSA project.
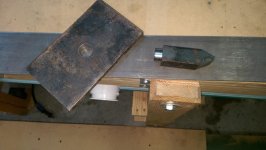
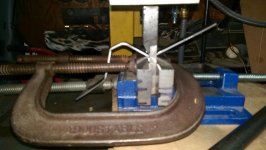
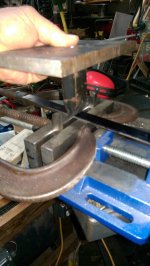
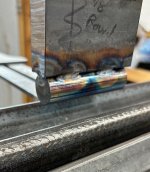
At the moment I’m unsure whether to bend the steel sheet (.062 is the thickest for now) using hammer blows or to bend by using pressure (brake).
Aircraft Spruce has some information which suggests the default is to pressure, if there is a dispute.
Is there a dispute? Some sources say NO to hammering, some say OK if done carefully.
I like Tony Bingelis’ descriptions and drawings which imply hammer blows (though I didn’t see where he says so explicitly).
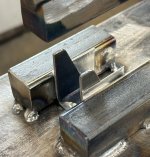
At the same time, there are some good ideas for making a simple brake for bending steel.
Also, some sources say the bend radius for our 4130 should be 3X the thickness.
Other sources say to bend around a diameter of 3X the thickness.
How did you bend your parts?
 

Attachments

  • photo18728.jpg
    photo18728.jpg
    156.1 KB · Views: 0
  • photo18729.jpg
    photo18729.jpg
    63.7 KB · Views: 0
  • photo18730.jpg
    photo18730.jpg
    147.9 KB · Views: 0
  • photo18731.jpg
    photo18731.jpg
    88.8 KB · Views: 0
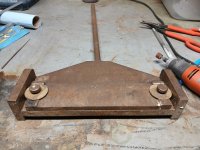
Here is my brake I built in the early 80's to plans in Sport Aviation. Works great on steel up to .100 thick. I build replacement dies with different bend radaii for different material thicknesses. Bud Davisson did an article in the March 2023 SA which summarizes everything. I highly recommend it.
Cheers
Gerry
Patrol#30
 

Attachments

  • 20250907_192556.jpg
    20250907_192556.jpg
    1.7 MB · Views: 0
  • 20250907_192522.jpg
    20250907_192522.jpg
    1.4 MB · Views: 0
  • 20250907_192544.jpg
    20250907_192544.jpg
    1.9 MB · Views: 0
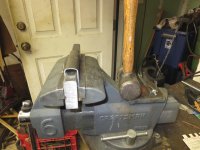
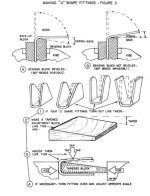
Thanks for the information, Gerry. I did see your previous post with this brake. And you also guided me to some interesting articles from the archives. When it comes to making the end pieces of the aileron support frame (3/4 inch inside the channels), the vise and bending blocks may be the most practical way to go. Unless a brake with a 3/4 inch hold down bar is devised.

Attached are three articles and a video link. From 2023 is the article you referenced (kudos to you and the photo credit). From 1967 is the drawing by Henry Karston. From 1966 is an article by Karston about 4130 steel fittings.

I'd like to continue to test my theory that scratch builders have more fun, and build a small but "manly" brake to be used for the various pieces needed for the project, even if it can't do the 3/4 inch channels.

Karston's drawing indicates machining I am not prepared to do. Attached is a link to a video which shows an approach I might be able to handle. If I can find the kind of hinges used in this video I will get some and give it a try.

https://www.youtube.com/watch?v=_LradMr1lz0
 

Attachments

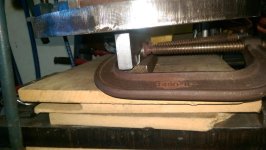
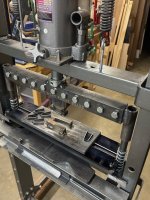
I made a 20 ton press some years ago.

This is my second harbor freight clamp. It will not survive without the other supporting clamps
s1.jpg
s2.jpg
s3.jpg

s4.jpg
s5.jpg
this bar has two sides ground to give a spring back for the 4130 steel
s6.jpg
s7.jpg
s9.jpg
 
For the wing hinges
I did it another way.


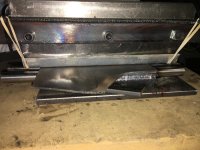
i welded some drill rod to a plate
I then made a guillotine blade that could bend the angle

Click image for larger version  Name:	b2.jpg Views:	0 Size:	243.5 KB ID:	97667


Click image for larger version  Name:	b2.jpg Views:	0 Size:	243.5 KB ID:	97667


The rubber band just holds a protective nose on the guillotine .


d1.jpg

d2.jpg

Click image for larger version  Name:	b2.jpg Views:	0 Size:	243.5 KB ID:	97667

d3.jpg
 

Attachments

  • b3.jpg
    b3.jpg
    233 KB · Views: 0
Last edited:
for the pulley bracket I made a different tool

c1.jpg
c3.jpg c4.jpg
 

Attachments

  • c3.jpg
    c3.jpg
    240.2 KB · Views: 0
  • c3.jpg
    c3.jpg
    240.2 KB · Views: 0
  • c2.jpg
    c2.jpg
    131.2 KB · Views: 0
I already had a 20 ton press with air over hydraulic bottle used to press out my wing ribs, so I picked up a finger brake kit from Swag Off Road for most of my fittings. I used a combination of:

- Bottoming dies with a fabricated upper die with desired bend radius ground in and tack-welded to the 5/8" thick die (finger) body
- Bending in the V-channel with the stock finger brake, and
- Air bends over Swag's bottom V-die and fabricated upper dies

Iin retrospect, a set of gooseneck dies for the brake could have handled some of the channel bends, but I got pretty good at tacking up bottoming dies, then grinding the welds back , knocking off the bar stock, and moving on to the next set of hardware to be fabricated.

Most steel cutting got done on a Hercules portable bandsaw (aka, Portaband, Milwaukee's trademarked name for their offering) set up on the Hercules table. If you already have a portable bandsaw, Swag and other folks have conversion tables, but the Hercules table also was set up to function as horizontal bandsaw. I routinely cut up to 3/4" plate and 1" bar stock in mild steel with it, so no issue on the thin stuff we use for the 4130 parts. Lots of scrap stuff at the local junk yard that just wants cleanup.

Between the finger brake ($~400), bottom V-die ($220), and about hundred or so in plate, rod, and angle stock, I spent about $900 on press stuff and took advantage of a one-time discount and big sale to pick up the portable bandsaw and table for about $200. A good 12" disk sander with 40 or 60 grit AlZr disks makes contouring upper does pretty fast... I have a 20" variable speed sander/grinder I use in guitar building, but a 12" is great for cleaning up profiles and edges sufficient to get them on a 3M wheel to polish out any scratches. There are less expensive versions of finger brakes for the various 12 and 20 ton presses such as HF, so def ways to cut costs.

Considering the setup has done two airplane's worth of hardware, I won't feel too bad seeing it go on Facebook marketplace. In the meantime, I find uses for the press and finger brake on a routine basis in my shop. Sort of like having a welder in the shop... as soon as you have one, there are always jobs to do.

Click image for larger version  Name:	IMG_0895.jpg Views:	0 Size:	77.1 KB ID:	97682 Click image for larger version  Name:	IMG_0897.jpg Views:	0 Size:	97.8 KB ID:	97683 Click image for larger version  Name:	IMG_0897.jpg Views:	0 Size:	97.8 KB ID:	97683 Click image for larger version  Name:	IMG_0897.jpg Views:	0 Size:	97.8 KB ID:	97683 Click image for larger version  Name:	IMG_0897.jpg Views:	0 Size:	97.8 KB ID:	97683 AileronBracketBrakeSetup.jpg Aileron Lwr FuseBracket.jpg
 
Last edited:
I do like using a press. 20 tons would be a minimum. Harbor freight sells -currently $250. You might be able to pick up one on Facebook marketplace or craigslist.

If I absolutely need a certain size of 1018 steel for dies I use onlinemetals.com. Try not to buy tool steel since you will spend the rest of your life trying to make a die.

Lately, I find that I can get what I need from amazon.com much cheaper. Individuals sell cutoff lengths at a more affordable price. Amazon is a good source for co-polymer plastic also.


The other harbor freight item for both steel and aluminum
Click image for larger version  Name:	e1.jpg Views:	0 Size:	1.50 MB ID:	97691
The belt sanders use to be $35 - they are more now. You would think such a rinky-dink thing would not be of much use but it turned out to be quite useful.

Sometimes you need to make a special one off tool. I find that 5/8 key-stock is cheap
Click image for larger version  Name:	e1.jpg Views:	0 Size:	1.50 MB ID:	97691

You can get 5/8 keystock from amazon.com but grainger has it for about $10 a foot - if you live near a Grainger.

Grainger also sells 3/4 x12 inch 1018 keystock for about $15.


I also get drill rod from amazon. Although drill rod can usually but procured at a machine shop.

I try to avoid home depot and lowes because the prices are ridiculous.
 
Last edited:
Amazon and Ebay tend to be pretty cheap if you shop carefully (watch those $10 pieces of steel with $35 ship cost!!!). I bought a couple 1/2" A-36 or 1008(?) plates to use as base pieces and a bunch of rod and bar stock from online and the scrap yard in Frederick. Absolutely agree on tool steel - we are making a dozen or less of something, so no need to do what we would do for hundreds or thousands of stampings.
 
Last edited:
I used parts from my wing spar brake to make a steel bender. The first version showed where it needed to be beefed up. The second version works pretty well on .040 and .063. I haven't tried it on the .090 and .100 yet, but I'm hopeful since those pieces are very narrow. The rest of the fabrication for these parts is basic band saw, file, grinder, sander and polisher. Here's a short video: https://youtu.be/KkGXux2vU1s​
 

Attachments

  • photo19021.jpg
    photo19021.jpg
    2.3 MB · Views: 0
  • photo19022.jpg
    photo19022.jpg
    2.5 MB · Views: 0
Those look great! .100 should be about 4x the bending load per inch of material versus .063, but that looks pretty beefy. Biggest issues are as you mentioned - bend radius and cracks. Had just one of the aileron pulley fuselage mount brackets crack, and that was in an area that would have been remelted into a weld had I not tossed it. The gear stuff is the big challenge... just saying.
 
Back
Top